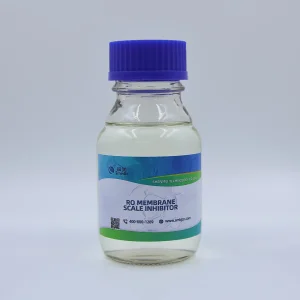
In the global industrial landscape, Reverse Osmosis (RO) systems are the backbone of water purification. As a leading manufacturer, Smedic Technology integrates E-E-A-T principles to provide high-performance antiscalant formulations. Our chemical engineering team ensures that every batch minimizes membrane fouling, thereby extending the lifecycle of RO modules and reducing operational downtime for industrial plants worldwide.
China has emerged as the global hub for water treatment chemical manufacturing. By leveraging advanced supply chain infrastructure and the integration of R&D with large-scale production bases (over 1 million tons annual capacity), we offer unparalleled cost-efficiency without compromising on quality.
Our formulas are developed in partnership with top universities to provide superior chelation and crystal modification, preventing even the most stubborn silica and calcium carbonate scaling.
Yes, with a network spanning China and logistics hubs in key regions, we offer efficient international shipping and technical support for large-scale projects.
 Smedic Tech